More cavities means more parts per shot — but also a bigger mold, a stronger machine and tighter demands on balance and cooling. A multi-cavity injection mold only pays off when cavity count is matched to your real volume and line. This guide shows how to size it, what it costs, and where buyers go wrong.
1. Output Math: Cavities × Cycle Time
Throughput is simply cavities × parts per cycle ÷ cycle time. Doubling cavities does not double output unless the rest of the line keeps up. Work backward from your required daily/monthly volume:
| Daily output need | Typical cavity choice | Best for |
|---|---|---|
| Pilot / R&D, low volume | 2 – 8 cavities | Sampling, market testing |
| Small–medium production | 16 – 32 cavities | Regional bottlers |
| High-volume water & CSD | 48 – 72 cavities | National brands |
| Ultra-high-speed lines | 96 cavities | Mega plants, 2-step systems |
Rule of thumb: choose the smallest cavity count that meets your required output with ~15% headroom. Over-cavitating is the #1 reason small buyers end up with a mold their machine cannot run efficiently.
2. Cost: Upfront vs Per-Part
A high-cavity mold costs more to build — more steel, more machining, a bigger hot runner, tighter balance work. But the per-part cost drops sharply because one cycle yields many parts. The crossover point is volume:
- Low volume: a 4–8 cavity tool is cheaper overall; a 48-cavity tool wastes capital.
- High volume: the higher tooling cost is repaid in months through lower cycle cost and labor.
- Machine fit: more cavities need more clamp force and plasticizing capacity — confirm before you buy.
3. Hot Runner Balance: The Make-or-Break Detail
In a multi-cavity injection mold, imbalance is fatal: if one cavity gets more melt than another, you get weight variation, short shots or flash. A balanced hot-runner with valve gates keeps every cavity within tight weight spread.
What to demand from any supplier:
- Hot-runner brand and gate type (valve vs open).
- Measured cavity-to-cavity weight variation (we target minimal spread).
- Cooling designed per cavity, not per mold, for repeatable cycle time.
4. Cycle Time & Cooling
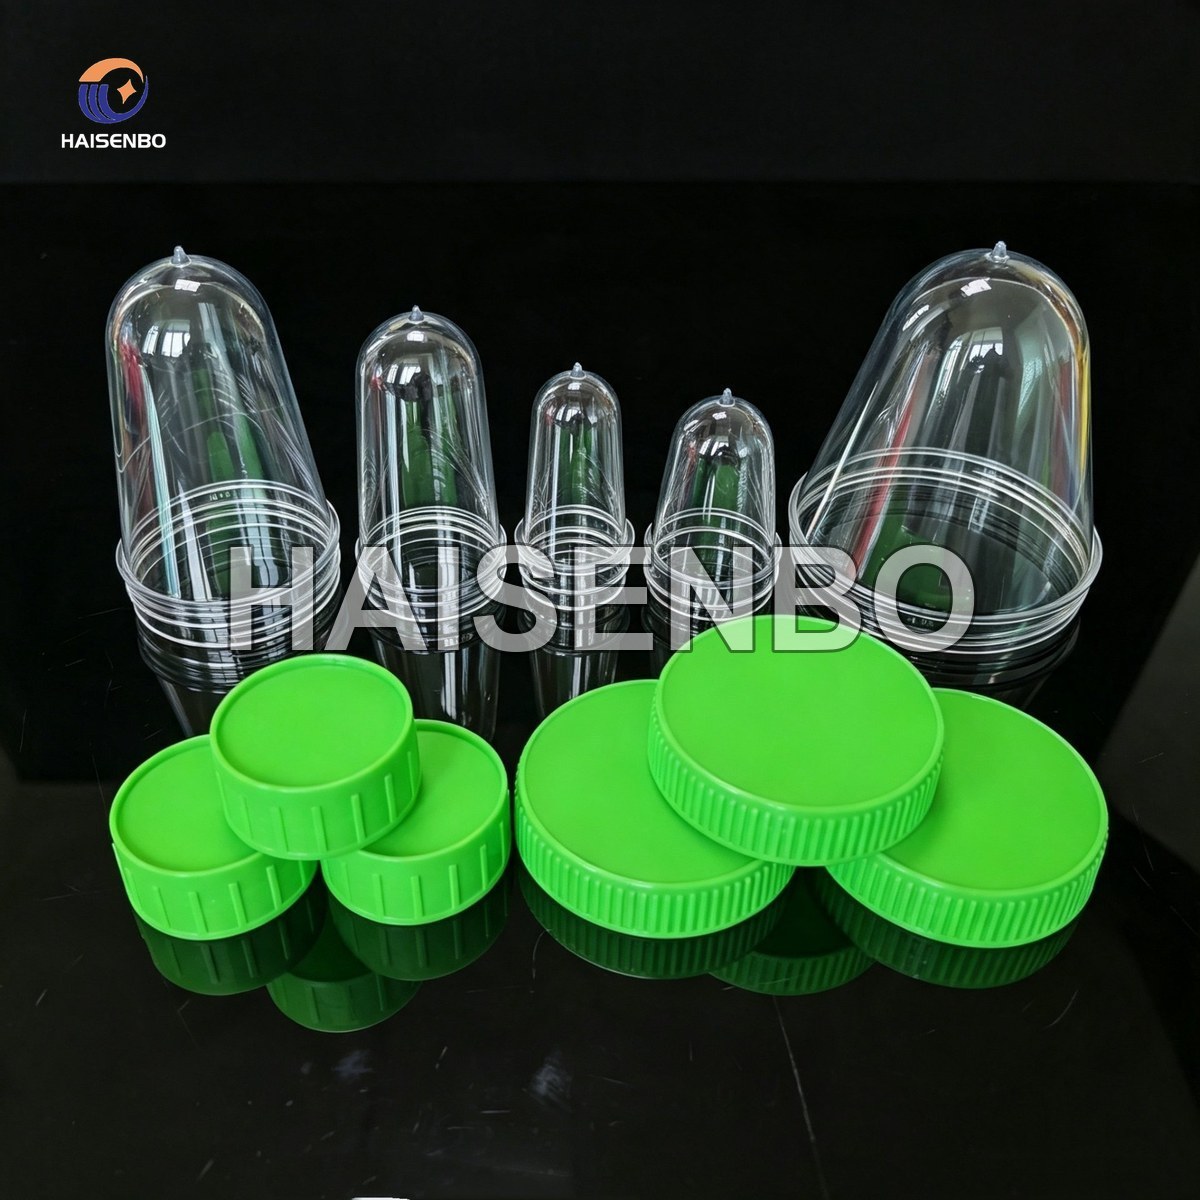
Cycle time is where a multi-cavity mold earns its keep — or loses it. Optimized, conformally-cooled channels let high-output tools hit cycle times as low as ~15 seconds on preform lines. Poor cooling means longer cycles that erase the cavity advantage.
5. Machine Limits You Must Check
- Clamp force: cavity count × projected area × melt pressure must stay under machine tonnage.
- Plasticizing: the screw must melt enough resin per cycle for all cavities.
- Platen & daylight: a 96-cavity tool is physically large — confirm it fits.
- Drying: resins like PET need adequate drying capacity upstream.
6. A Quick Sizing Checklist
- Volume first: size cavities to real output + 15% headroom.
- Machine check: verify clamp, plasticizing, platen.
- Hot runner: insist on balanced valve-gate + measured variation.
- Cooling: per-cavity optimization for cycle time.
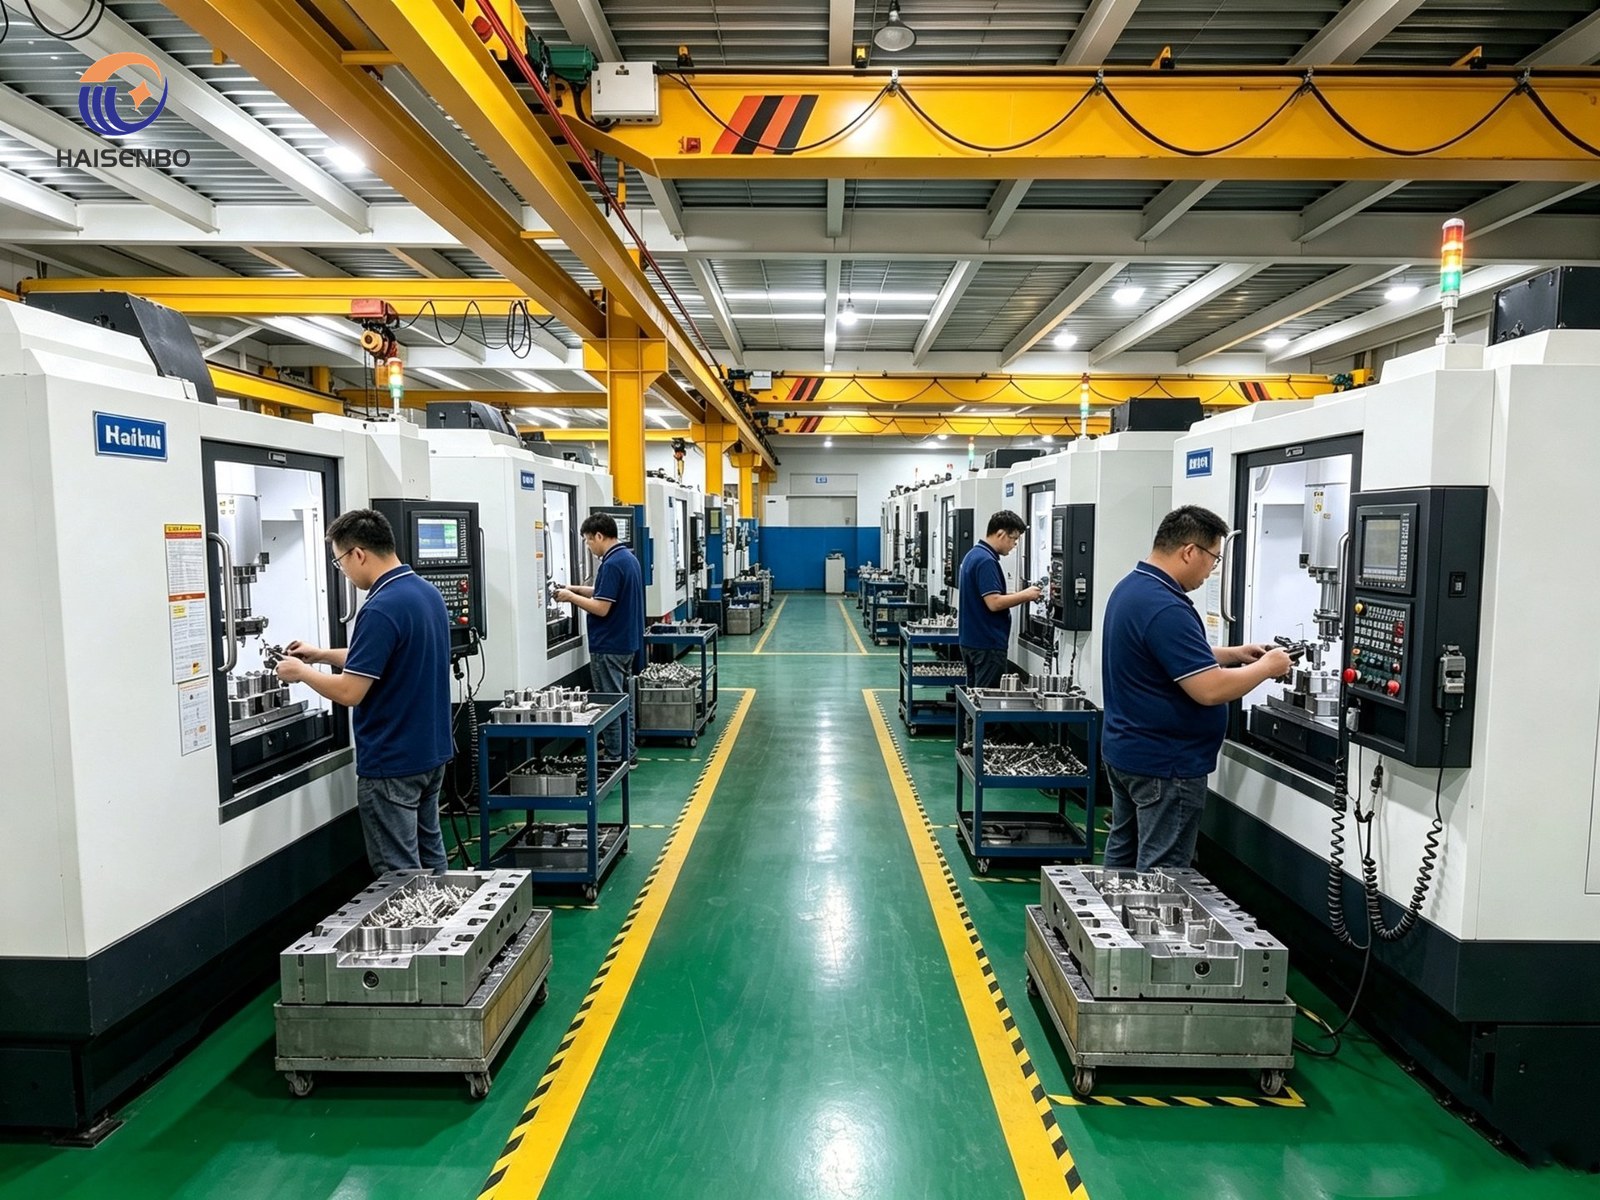
- Steel: S136H / 2344 cores & cavities for 3,000,000+ shots.
- Tolerance: written spec + CMM report.
With 30+ years and 10,000+ molds delivered to 60+ countries, Haisenbo builds multi-cavity injection molds from 2-cavity development tools up to 96-cavity high-speed production molds on one proven platform. See our factory or browse all products.
If you want cavity count and steel sized to your line, reach out for a free quote — our engineers usually respond within 24 hours.